
What Should Buyers Check for Connector and Interface When Sourcing Fiber Optic Connector?
 FIBERXI
 FIBERXI
Introduction
Confirm the exact connector interface from the mating port, including format, polish, gender, keying and adapter compatibility, before deciding on a connector part number. A dependable buying decision starts with the installed application, not a product photo or a broad compatibility claim. For a B2B order, the buyer should make the equipment interface, route condition, required quantity, inspection method and receiving plan visible before quotation.
At FiberXi, requirement reviews commonly begin with the project drawing, existing part number, port photograph or item list. This helps separate a standard repeat SKU from a configuration that needs engineering confirmation. It also gives factory testing and shipment inspection a specific reference instead of a verbal expectation.
Direct answer for buyers
The best way to source fiber optic connector is to confirm the use case first, write the technical configuration second, and compare supplier responses on the same release basis. A low price is not comparable if the fiber, connector, cable construction, labels, test scope or packing plan is different.
Use a controlled purchasing sequence
1. Identify the real application
Record where the fiber optic connector will be installed, what it mates with, how it will be routed and who will accept it. A data-center rack, a subscriber drop, an outdoor duct and a telecom cabinet can all use optical products, but they create different requirements for fiber, protection, handling and documentation.
2. Translate the application into a specification
List the decisions that affect fit, optical performance or installation time. Avoid words such as "standard," "high quality" or "compatible" unless a part number, drawing, data sheet or measurable acceptance criterion supports them. The release should also show which details are fixed and which can be proposed by the supplier.
3. Confirm the delivery and acceptance plan
Decide whether goods will be inspected by item, batch, drum, carton or shipment. Include buyer part numbers, label text, accessory packs and carton marks where the receiving team needs them. For staged projects, group goods by site, cabinet, rack or deployment phase when that reduces handling risk.
Key checks before issuing an RFQ
| Check | What to review | What to document |
|---|---|---|
| 1 | LC, SC, FC, ST or MPO/MTP format | Put the agreed choice in the RFQ, drawing or release table. |
| 2 | UPC/APC polish and color convention | Put the agreed choice in the RFQ, drawing or release table. |
| 3 | Simplex, duplex or multi-fiber orientation | Put the agreed choice in the RFQ, drawing or release table. |
| 4 | Adapter, panel and enclosure compatibility | Put the agreed choice in the RFQ, drawing or release table. |
Product-specific design context
A connector is a matched optical interface
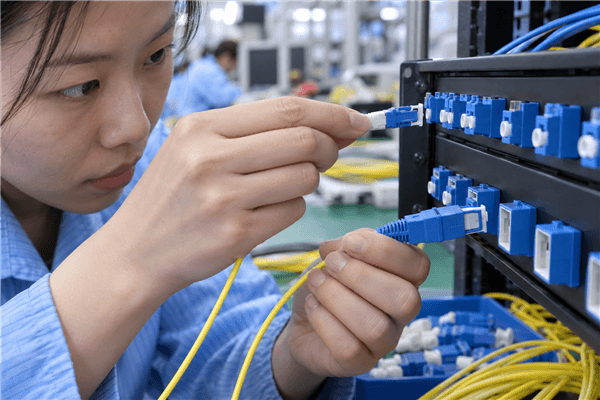
Connector selection begins with the mating component: equipment port, adapter, panel, cassette, pigtail or field-termination hardware. The connector family alone is not a complete specification. Buyers also need to establish fiber compatibility, ferrule format, polish, simplex or duplex orientation, keying and the termination method. A clear mating-part number or a sharp port and adapter photograph can prevent an incorrect assumption before a purchase order is issued.
End-face control affects system reliability
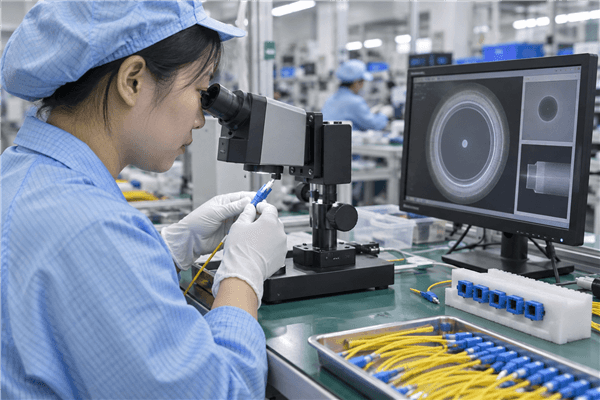
The product must arrive with the specified finish, appropriate protection and a testable assembly process. Connector cleanliness, end-face condition and correct pairing matter during both factory testing and field work. Ask how identification is maintained across the connector, adapter and finished assembly. Where a connector is supplied as part of an assembly, confirm whether the inspection record applies to the assembly or to a component sample.
Confirm the field workflow before buying components
For field termination, consider the tools, preparation steps, training and access conditions at the installation site. For factory-terminated assemblies, focus on the mating standard, cable interface, boot clearance and packing protection. Either approach can be appropriate; the practical choice depends on schedule, repeatability, labor conditions and the project acceptance plan. The request should state which workflow the site has approved rather than leaving the supplier to infer it.
Detailed guidance: Interface
Interface control starts at both sides of the connection. Record the actual mating ports, adapters, panels or enclosures—not just a familiar connector name. The release should identify connector family, polish, orientation, polarity or keying where relevant, and any physical-clearance issue around the port. A photograph with a part number is often more useful than an email description when an installation uses legacy hardware or a high-density panel.
Do not use color alone to decide polish or fiber system. Confirm the requirement against the connected equipment and project documentation. When a multi-fiber or duplex assembly is involved, map end A to end B and document the expected orientation before assembly. The practical items to check are LC, SC, FC, ST or MPO/MTP format; UPC/APC polish and color convention; Simplex, duplex or multi-fiber orientation; Adapter, panel and enclosure compatibility.
During receiving inspection, examine protective caps, labels, mating-end condition and the configuration on the outer pack before units are distributed. During installation preparation, use the approved cleaning and inspection process. This is a sensible control because a correct factory assembly can still be affected by handling, contamination or incorrect routing at site.
Turn the review into an actionable release plan
Build one source of truth before production
The purchasing order, technical drawing and packing instructions should point to the same approved configuration. For fiber optic connector, a practical release package has a buyer item number, revision date, plain-language product description, the agreed mating interface, polish, orientation and physical clearance, quantity and delivery grouping. Attach the source material used to make decisions: route data, end-port photographs, equipment data, panel drawing, sample sign-off or customer specification. This is not paperwork for its own sake. It prevents an assembly team, test operator and shipping team from receiving different verbal instructions.
Where the buyer cannot yet confirm a detail, mark it clearly as an open point with an owner and decision date. Do not put “TBD” into a production release without a rule for what happens if the decision is late. The supplier can then identify the latest point at which the missing information will affect materials, tooling, lead time or inspection. This gives purchasing a realistic choice: resolve the point, approve a documented assumption, or move that item to a later delivery phase.
Make factory testing and receiving inspection complement each other
Factory testing should prove the agreed product configuration at the factory; receiving inspection should confirm that the approved goods and records arrived in usable condition. Divide responsibilities explicitly. For example, factory controls may include configuration check, visual workmanship, agreed optical measurement, label verification and packing review. Receiving controls may include carton count, buyer part number, protective caps, condition of packaging, document match and any site-specific check before installation. The appropriate sampling level depends on the product and contract, so state it rather than implying that a generic test certificate covers every risk.
When a result is outside the agreed condition, request a nonconformance description that identifies the item, quantity, observed issue, disposition and corrective action. This is more useful than a broad assurance that the shipment has been “rechecked.” It preserves traceability and helps decide whether replacement, sorting, rework or a documented concession is suitable. For recurring fiber optic connector orders, review the pattern of issues as part of supplier performance rather than treating each shipment in isolation.
Protect the project from uncontrolled changes
Changes often begin with a reasonable commercial request: a different cable color, connector source, label layout, carton size, reel schedule or dispatch split. Some changes are harmless; others can change installation compatibility, acceptance evidence or inventory identification. Require a written change notice that names the affected item, previous revision, proposed revision, reason, impact on price and lead time, and required buyer approval. No change should be assumed acceptable because it appears visually similar.
At the end of the project, retain the final approved release, inspection records, packing list and any change notices. That record turns the next inquiry into a controlled repeat order and makes future troubleshooting faster. It also gives both parties a credible evidence trail when customer requirements, installation conditions or receiving procedures evolve.
Technical context that should not be guessed
Fiber selection and installed bend behavior should follow the network requirement. ITU-T G.652 is the current ITU-T recommendation for single-mode optical fiber and cable characteristics. For access and high-density routes, ITU-T G.657 describes bend-loss-insensitive single-mode categories; the project standard and actual route remain the controlling requirements.
Installation preparation is part of product selection. The FOA Installation Standard advises testing fibers with an optical loss test set against the calculated loss budget and inspecting connector cleanliness and damage before testing or connection. These principles are useful procurement controls, but the buyer should still define the exact product-specific test method, wavelength, reference condition and acceptance criteria.
What to request from the supplier
- Port or adapter image
- Interface part number
- Polish and keying
- Assembly or termination method
Ask the supplier to identify missing information before production is released. This is more useful than accepting assumptions after an order is issued. For a new configuration, a controlled sample, first-article review or drawing approval may be appropriate before a larger project quantity is scheduled.
Testing, inspection and shipment control
Testing should be relevant, traceable and agreed in advance. Depending on the product, the order may need configuration verification, visual inspection, length or dimension checks, label confirmation, connector-end condition, optical measurements or cable test records. State whether evidence is required per item, batch, reel or shipment.
During shipment inspection, compare quantities, buyer part numbers, protective caps, accessory packs, labels and carton marks against the approved packing list. A technically correct product can still slow installation if labels do not match the receiving plan or if the right accessory is packed in the wrong carton.
Common buying mistakes
One common mistake is asking for a quotation without identifying the mating interface or installed environment. Another is comparing two prices when one supplier includes a different cable construction, test scope or packing method. Buyers also lose time when label artwork, carton marks and documentation are defined only after production is complete.
Use one approved release package for repeat orders. It should hold the product description, drawing revision, label text, packing rule, inspection requirement and change-approval contact. This creates an auditable handoff between purchasing, production, shipment inspection and the receiving team.
FAQ
What information is most useful in a first inquiry?
Send an existing part number, product image, port photograph, drawing or concise application description. Add quantity, destination, required delivery timing and the details already known. This lets the supplier identify the missing configuration points before quoting.
Can fiber optic connector be customized?
Many fiber optic products can be configured around interfaces, fiber category, dimensions, length, labels, packaging and accessories. Feasibility, MOQ and lead time should be confirmed against the final approved configuration rather than assumed from a generic item.
How should buyers compare quality?
Compare the same approved configuration, material and test basis. Check the product data sheet, sample or drawing, inspection method, record identification, packing protection and how repeat orders will be controlled. General quality claims are not an acceptance standard.
What should be reviewed before shipment?
Review ordered configuration, quantities, labels, accessories, inspection records and carton marks against the approved packing list. For project orders, verify that the grouping matches the site, cabinet, rack or phase plan.
Conclusion
Good sourcing for fiber optic connector interface selection depends on making the application and acceptance criteria explicit before manufacturing begins. A clear release package, relevant factory testing and disciplined shipment inspection help the buyer receive a product that can be installed and maintained with fewer avoidable questions.